How Organic molybdenum friction modifiers reduce friction in lubricants
Why can a small treat addition change friction behavior when an oil film becomes too thin to keep opposing metal surfaces apart? The answer is not simply that molybdenum is “slippery.” Organic molybdenum friction modifiers are oil-soluble precursor chemistries that can react at loaded, sliding contact zones and create a surface-derived film with low shear resistance. That film is most relevant during boundary lubrication, when base-oil viscosity alone cannot prevent asperity contact.
For engine-oil and industrial-lubricant formulators, the practical question is whether the chemistry can activate in the intended system, remain compatible with the rest of the additive package, and demonstrate repeatable friction behavior under relevant test conditions. A friction modifier may reduce measured friction in one test but show little benefit in another if temperature, load, sliding speed, metallurgy, base oil, or companion additives change.
This article separates the mechanism from the selection work. It explains what organomolybdenum chemistry does at a rubbing interface, which factors control the response, and how to assess results without treating one friction test as a universal prediction. For related product families, see our organic molybdenum friction modifiers page.
Friction reduction depends on reaching boundary lubrication
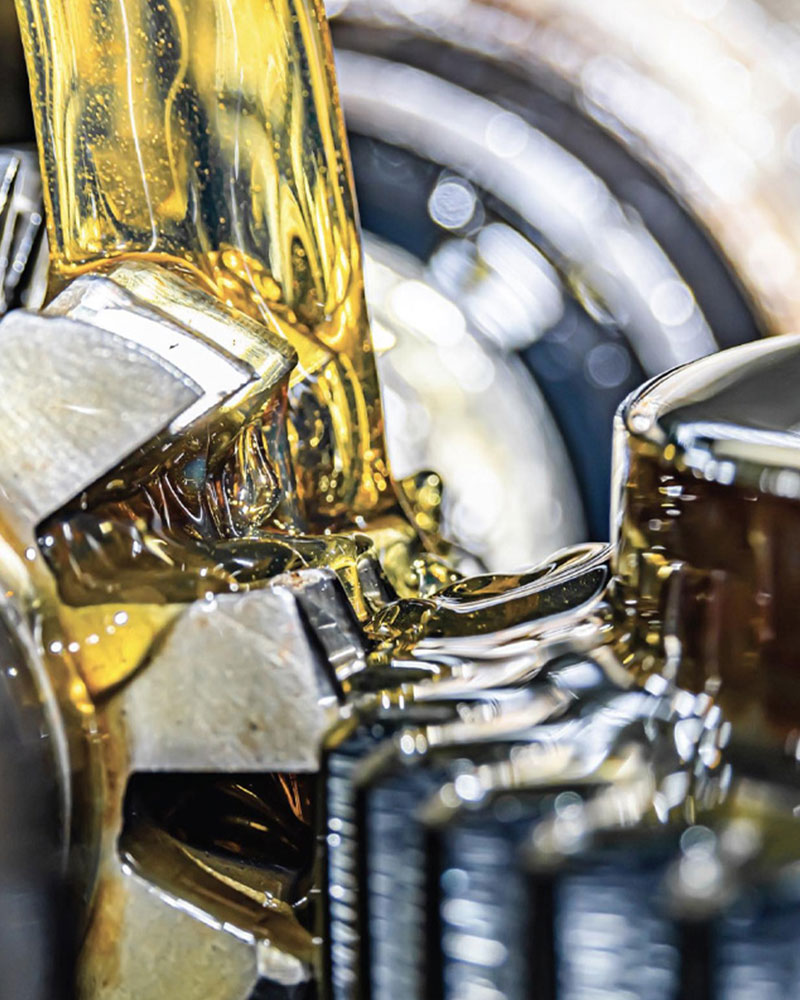
The direct answer is that an organomolybdenum additive can lower friction after it reaches a highly stressed rubbing contact and forms a low-shear reaction film. The chemistry is most useful when the lubricant operates in mixed or boundary regimes, rather than in full-fluid-film conditions.
Under hydrodynamic lubrication, a sufficiently thick oil film separates the surfaces. Friction is dominated largely by viscous drag within the fluid. In that regime, changing a boundary friction modifier may not produce a large benefit because metal asperities are not making meaningful contact. Under mixed lubrication, the fluid film carries part of the load while asperities carry the remainder. Under boundary lubrication, surface interactions become dominant, and additive-derived films can have a major effect.
| Lubrication condition | What controls friction most | Expected role of organomolybdenum chemistry | Selection limit |
|---|---|---|---|
| Hydrodynamic | Base-oil viscosity and fluid shear | Usually secondary because surfaces remain separated | Do not select a friction modifier as the main solution to excessive viscous drag |
| Mixed lubrication | Oil-film thickness plus asperity interaction | Can reduce friction where intermittent surface contact occurs | Benefits depend strongly on speed, load, temperature, and surface finish |
| Boundary lubrication | Surface chemistry, load-bearing films, and sliding behavior | Often highly relevant because low-shear tribofilms can form at contact points | It must still be compatible with antiwear, EP, detergent, dispersant, and corrosion-control chemistry |
Selection conclusion: consider this chemistry when the target component spends meaningful time in mixed or boundary lubrication, such as loaded sliding contacts, start-stop conditions, or contacts exposed to fluctuating speed and load. The reason is straightforward: a low-shear surface film matters only where the surfaces approach closely enough to interact. It does not replace viscosity selection, mechanical design, cooling, filtration, or a suitable antiwear and extreme-pressure strategy.
For industrial formulators, friction reduction and wear protection should also be separated. A lower friction coefficient does not automatically prove a stronger load-carrying system. Likewise, good PB/PD performance in a four-ball extreme-pressure assessment does not by itself establish low friction in an SRV test. Each method imposes its own contact geometry and conditions.
How organomolybdenum additives form low-shear tribofilms under boundary-lubrication conditions
Organomolybdenum compounds enter the lubricant in an oil-soluble form. During loaded sliding, local pressure, temperature, and surface activity can promote chemical transformation near the contact. The additive-derived species adsorb and react at the rubbing interface, building a tribofilm rather than remaining only dissolved in the bulk oil.
The resulting film may contain molybdenum-containing reaction products with layered, low-shear characteristics. When opposing asperities slide, shear can occur more readily within or along this film than through direct steel-to-steel contact. That reduces the tangential force required for sliding, which is measured as lower friction under the specific test conditions.
| Mechanism stage | What occurs at the contact | Practical consequence | What can change the outcome |
|---|---|---|---|
| Transport | Additive molecules move with the oil toward the rubbing zone | The chemistry is available where contact begins | Base-oil solvency, additive solubility, filtration, and bulk concentration affect availability |
| Adsorption and activation | High-energy surface sites, heat, and pressure encourage surface interaction | The additive can become concentrated at the contact rather than staying uniformly distributed in oil | Contact temperature, load, sliding severity, metallurgy, and existing films influence activation |
| Tribofilm growth | Reaction products accumulate on the rubbing surfaces | A protective, low-shear interface can develop | Competition from antiwear agents, detergents, dispersants, or reactive EP additives may alter film composition |
| Film removal and renewal | Sliding removes part of the film while fresh chemistry replenishes it | Steady friction behavior depends on a balance between formation and wear-off | Very severe conditions may remove film faster than it can reform |
Technical conclusion: friction reduction is a dynamic film-formation process, not a permanent coating applied before service. This distinction matters when comparing candidates. A candidate that performs well after an extended conditioning period may not behave the same way during short-duration operation, cold operation, or rapid load changes. Ask whether the test records friction over time, not only a single final value.
The film is also not an excuse to ignore the rest of the formula. In a finished engine oil, a molybdenum friction modifier can interact with detergent systems, dispersants, antioxidants, antiwear agents, viscosity modifiers, and base oils. In industrial lubricants, the interaction may include sulfurized EP chemistry, phosphorus-containing additives, rust inhibitors, and demulsifier requirements. If the formula needs extra antiwear or load-carrying support, review oil-soluble phosphate ester EP additives as a separate chemistry family rather than assuming the friction modifier performs every function.
Which formulation variables control friction response
The most useful way to evaluate an organomolybdenum candidate is to treat it as one part of a system. Higher addition is not automatically better. More chemistry may change friction response, but it can also affect solubility, storage behavior, ash-related constraints, cost, or compatibility with other additives. The correct choice is the lowest addition that produces acceptable behavior in the intended formula and test sequence.
- Base-oil composition: Base oils affect additive solubility, film thickness, oxidation stability, and molecular transport to the contact. Use the final base-oil slate during screening where possible. A result from one base oil may not transfer directly to another.
- Surface metallurgy and finish: The contact surface influences adsorption and reaction pathways. Steel-on-steel data should not be treated as proof for every alloy, coating, or surface treatment.
- Temperature: Temperature can support chemical activation, but it also changes oil viscosity, oxidation rate, and the behavior of companion additives. A better high-temperature result does not guarantee a better low-temperature result.
- Load and sliding motion: Oscillating sliding, rolling-sliding, and continuous sliding create different contact environments. Select a method that resembles the intended contact rather than relying on a convenient general screen.
- Companion antiwear and EP additives: These can complement the friction modifier by protecting loaded contacts, or they can compete for the same surface. Package screening is required to identify the net result.
- Antioxidant system: Friction performance must be considered alongside oxidation control, especially where thermal stress can affect the useful life of the lubricant. A friction result without oxidation assessment is incomplete for long-drain or high-temperature duties.
Recommendation for engine-oil work: screen friction behavior in the final or near-final detergent, dispersant, antiwear, and antioxidant environment. The reason is that engine oils are chemically crowded systems. This approach fits formulators replacing an imported component or modifying an established package. It is less necessary during an early raw-material solubility screen, but it becomes necessary before making performance claims.
Recommendation for industrial gear or hydraulic oils: first determine whether the main problem is friction, wear, scuffing resistance, corrosion, foam, or oxidation. The reason is that the corrective chemistry differs by failure mode. If high friction is accompanied by inadequate EP performance or large wear scars, a friction modifier alone may be insufficient. In such cases, assess it alongside appropriate industrial gear oil packages and the needed component additives.
How to verify a friction-reduction claim before selecting a chemistry
A low friction coefficient is meaningful only when the test conditions are disclosed. SRV testing is useful for controlled sliding-contact comparison, but an SRV result is not interchangeable with four-ball wear, four-ball PB/PD, oxidation testing, field operation, or fuel-economy testing. Each result answers a different question.
- Define the contact problem. State the component, material pair, motion type, expected temperature range, load behavior, and base-oil viscosity grade. This establishes whether the concern is boundary friction, wear, EP capacity, or bulk-oil drag.
- Prepare a control formula. Use the same base oil and additive package without the candidate friction modifier. Without a control, a lower value cannot be attributed confidently to the candidate chemistry.
- Test more than one treat level. Compare a small formulation series rather than only one dose. Record solubility and appearance during preparation and after storage. Do not assume a larger dose will keep improving the result.
- Record the full test method. Keep the contact material, load, temperature, frequency or speed, duration, specimen finish, and conditioning procedure with the result. These details determine whether two datasets can be compared.
- Pair friction data with wear and load data. Measure the relevant wear scar or surface condition and use an appropriate load-carrying assessment where the application demands it. Lower friction with unacceptable wear is not a successful formulation.
- Check oxidation and compatibility. Examine whether the new chemistry changes oxidation behavior, corrosion protection, foam, demulsibility, or other formula requirements. A good friction number is only one decision input.
- Inspect used surfaces when possible. Surface analysis can help distinguish film formation from random test variation. This is especially useful when two chemistries give similar friction values but different wear behavior.
Verification conclusion: compare results only when the test method and formula context are aligned. This procedure fits early technical evaluation and import-substitution work. It does not replace application-specific qualification testing, because laboratory contacts cannot reproduce every field contaminant, duty cycle, or thermal event.
Common interpretation errors that lead to poor additive decisions
- Treating a friction modifier as an EP additive. A low-shear film can reduce friction, while EP additives address severe load and anti-scuff requirements through different mechanisms. When PB/PD targets are not met, investigate the EP system instead of adding friction modifier without a plan.
- Comparing different test methods as if the numbers match. An SRV friction value and a four-ball wear result measure different outcomes. Use each test for its intended decision, then build a balanced performance picture.
- Ignoring the running-in period. Tribofilms may need time to form. Compare friction traces over the same duration and conditioning history rather than comparing isolated readings.
- Assuming a single-additive result survives package blending. Surface-active additives can interact. Retest after introducing the full package, including corrosion inhibitors where relevant, such as thiadiazole-based metal corrosion inhibitors.
- Using a friction result to claim longer lubricant life. Friction behavior and oxidation resistance are related only through the whole formula and operating conditions. Verify oxidation separately.
- Focusing only on the final coefficient. A stable trace, acceptable wear response, and repeatability across runs often provide more decision value than one low endpoint.
A practical example illustrates the issue. Suppose an industrial lubricant shows excessive sliding friction in a bench test, but it also produces a large wear scar and misses the required load-carrying result. Adding an organomolybdenum candidate may lower the friction trace, yet the formula can still fail its service target if the antiwear and EP system remains inadequate. The appropriate action is to keep the friction candidate in the formulation screen while separately adjusting the load-protection system, then retest the finished formula under matched conditions.
How to source and screen a suitable additive partner
For a development program, request technical information that supports a controlled comparison: recommended application area, compatible base-oil types, handling guidance, additive form, test methods used, and the limits of the available performance data. If the intended product is an additive package rather than a single component, clarify whether the supplier’s information applies to the individual component or the finished blend.
Luoyang Fangshan Chemical Co., Ltd. was established in 2017 and manufactures lubricant additive components and packages for global markets. The company reports functional-chemical production capacity exceeding 10,000 tons and an R&D team with more than 30 PhD and master’s degree holders. Its management systems include ISO 9001:2015, ISO 45001:2018, and ISO 14001:2015. These are useful supply and quality-management signals, but they do not replace formula-specific laboratory validation.
For screening projects, the company states that samples can be dispatched within 3 days and bulk orders within 7 days, with no MOQ. Those arrangements can help a formulator prepare a small comparison matrix before scaling up. Product-quality concerns are handled through return discussions by mutual agreement. The sensible next step remains the same: test the candidate in the final intended formulation and against the performance criteria that matter for the end-use lubricant.
Request selection advice or a sample for a controlled comparison in your engine-oil or industrial-lubricant formulation.
 WhatsApp
 Email
 +8616638861155